Premade pouch fillers
For existing pouch formats where opening, dosing, sealing and presentation are central.
View route →Compare premade pouch filling, VFFS bagging, sachet-style liquid filling and integrated filling & sealing machinery for real production requirements.
A good pouch-filling shortlist starts with product flow, pouch style, seal quality, target output and integration requirements rather than a generic machine list.
For existing pouch formats where opening, dosing, sealing and presentation are central.
View route →For bag-forming lines using roll film where throughput and repeatable seals matter.
View route →For auger, weigh-head, multihead and dry-product filling applications.
View route →For sauces, oils, gels, cosmetics and chemicals in flexible packs.
View route →Selected pouch, VFFS and filling & sealing systems using media paths from Lancing UK source websites.
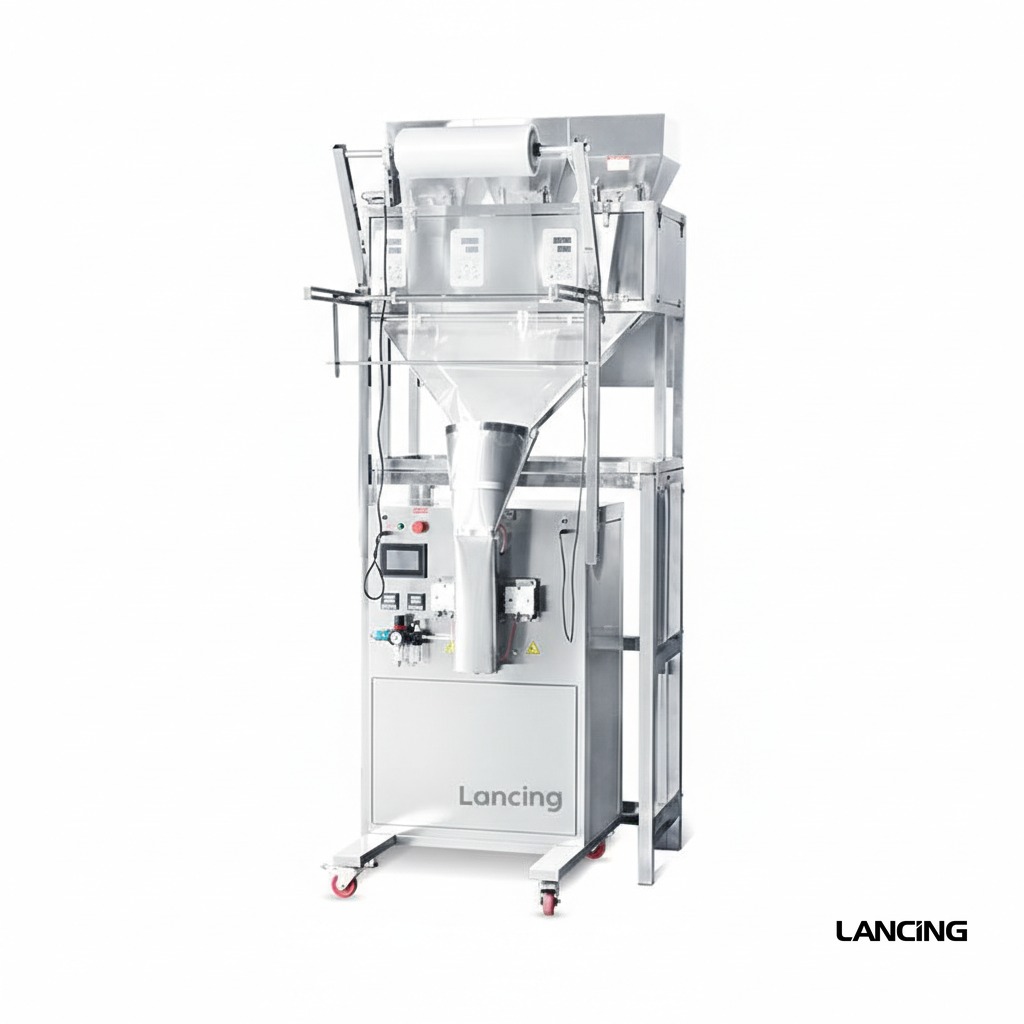
Compact pouch weighing, filling and sealing route for granules and free-flowing products where a neat finished bag is required.
Back-seal granule pouch filling and sealing system for higher bagging speeds with adjustable product and film formats.
VFFS auger filling and sealing system built around powder behaviour, clean dosing and dust-control considerations.
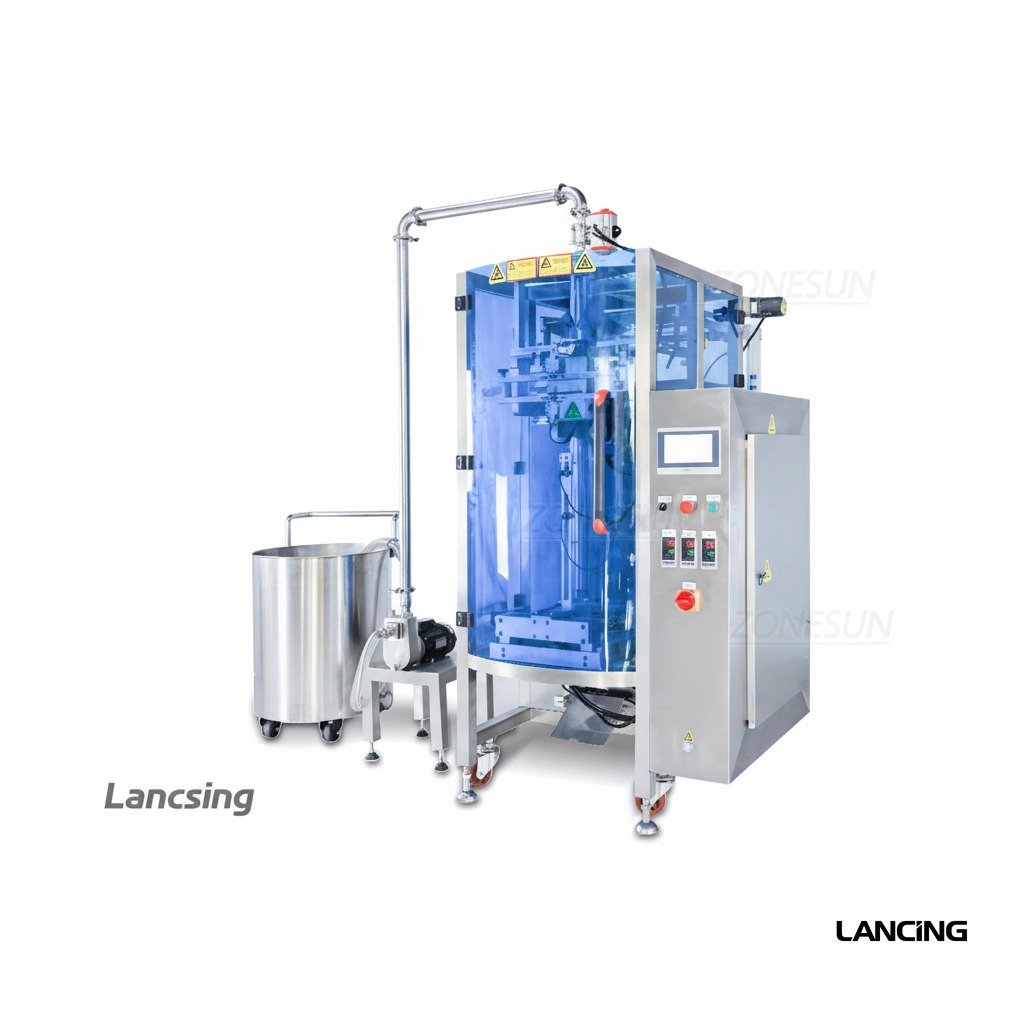
Automatic pouch filling and sealing route for liquid and paste products with configurable tanks, pumps and film widths.
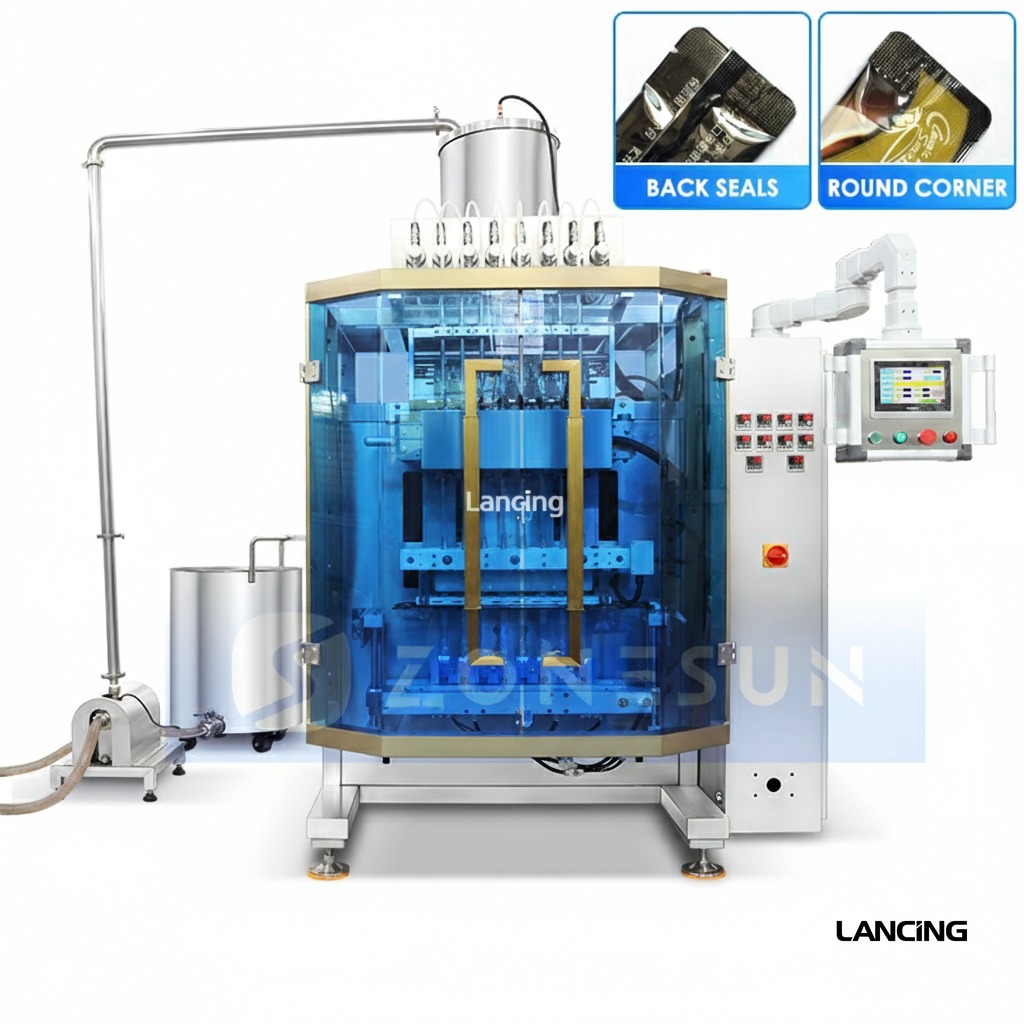
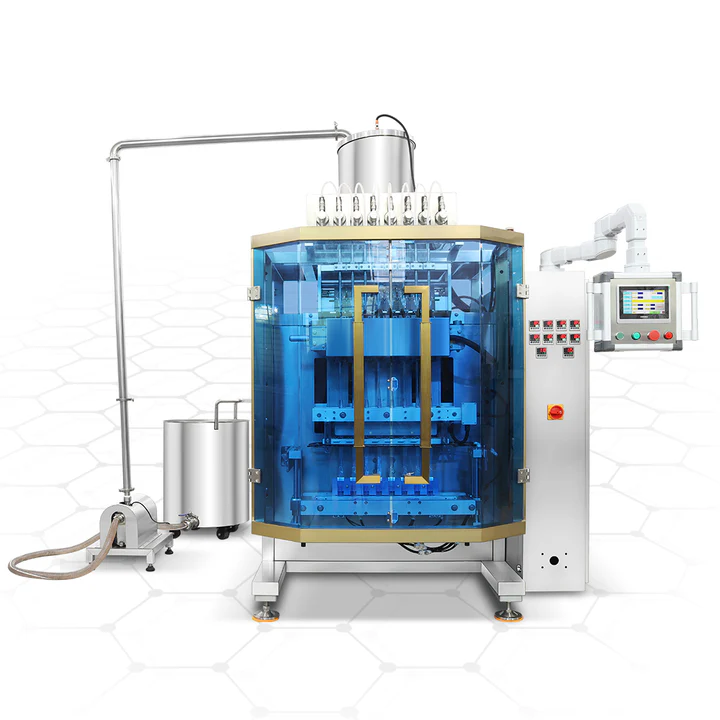
Eight-channel VFFS liquid bagging system for small-format liquid pouches where repeatability and output are key.
Start by separating the decisions already fixed from those still open. An approved premade pouch with a zipper or spout constrains handling differently from a pack that can be formed from roll film. Product behaviour then determines which dosing arrangement can work within that packaging route.
Use production samples to assess pickup, opening, gripping area and access for the dose. Include the smallest usable mouth and the highest intended fill. A nominal pouch width does not establish that a nozzle or product chute can enter without damaging the pack or contaminating its closing area.
Compare the complete product path before choosing the number of filling heads. Cohesive powder, fragile granules, a foaming liquid and a paste with pieces create different feed, discharge and cut-off questions. Retain observations at replenishment and restart as well as during stable running.
Inspect the pouch immediately before sealing. Product trapped at a zipper, dust on a sealing surface or liquid trailing after nozzle withdrawal may require a handling or timing change. Increasing the dosing rate cannot solve a closing area that is not ready.
Observe support, orientation, cooling where relevant, inspection and discharge. A filled pouch may change shape or stability, so the empty-pack trial is not enough. Define the handover to the next operation and the response when that operation stops.
Compare accepted finished packs and the reason for each loss. This keeps the shortlist focused on the limiting operation while the detailed guides below address opening, sealing, inspection and integration.
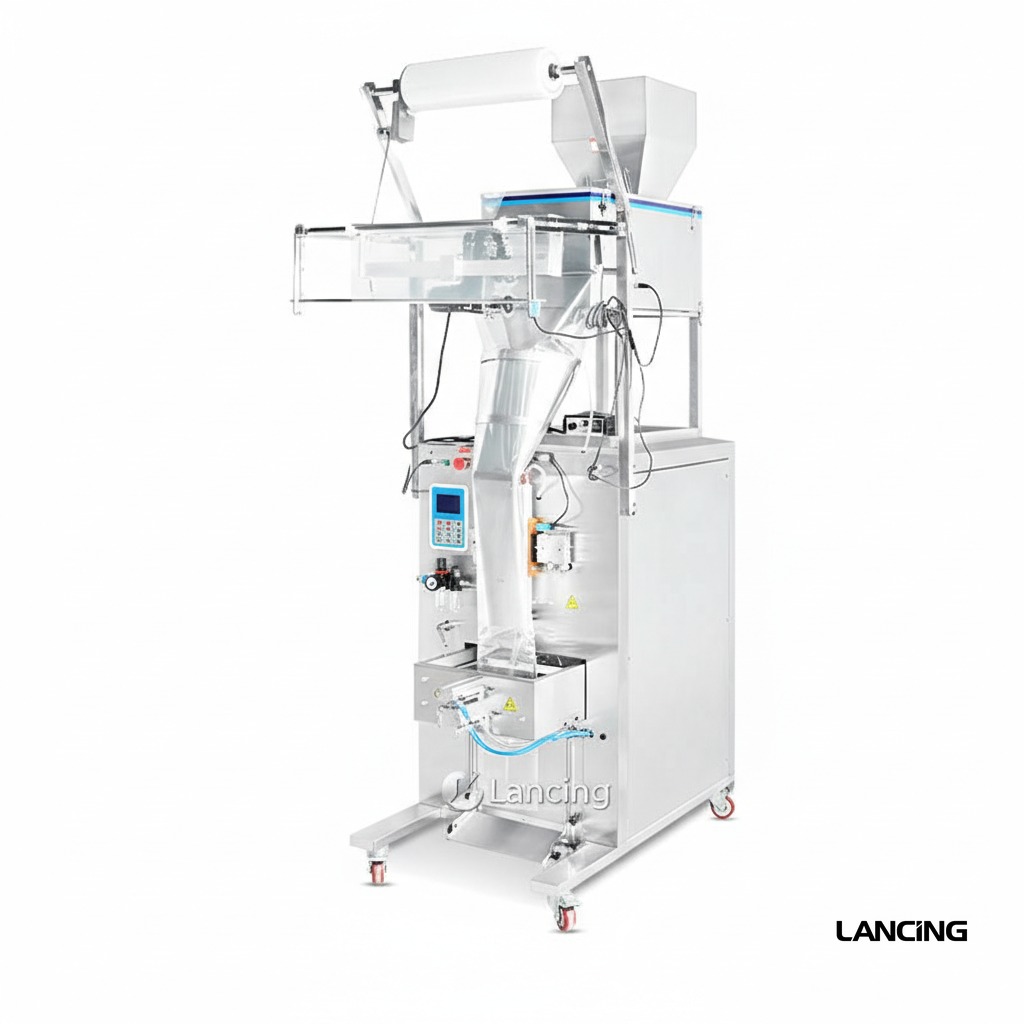
Send the product type, fill weight or volume, pouch material and dimensions, target output, seal style, available utilities and any coding or checkweighing requirement.
Usually the dosing system is selected around one main product behaviour. Powders, granules, thin liquids and viscous pastes normally need different filling principles.
Often yes. Coding, checkweighing, discharge conveyors, secondary packing and inspection should be considered early so the full line works as one process.
We’ll help shortlist whether a premade pouch machine, VFFS bagger, auger, multihead weigher, piston pump or multi-channel liquid system is the practical route.
Doypack describes a stand-up pouch format; it does not by itself identify the dosing system or every handling requirement. Compare the finished pouch features with the way the machine receives packaging, fills it and closes it.
Premade pouch machines handle supplied pouches before filling and closing. Start with the mouth, gusset, zipper or spout and the variation in production samples. Confirm separation, opening and gripping before judging dose speed. An attractive empty pouch is not evidence that it can be opened and filled consistently on the proposed machine.
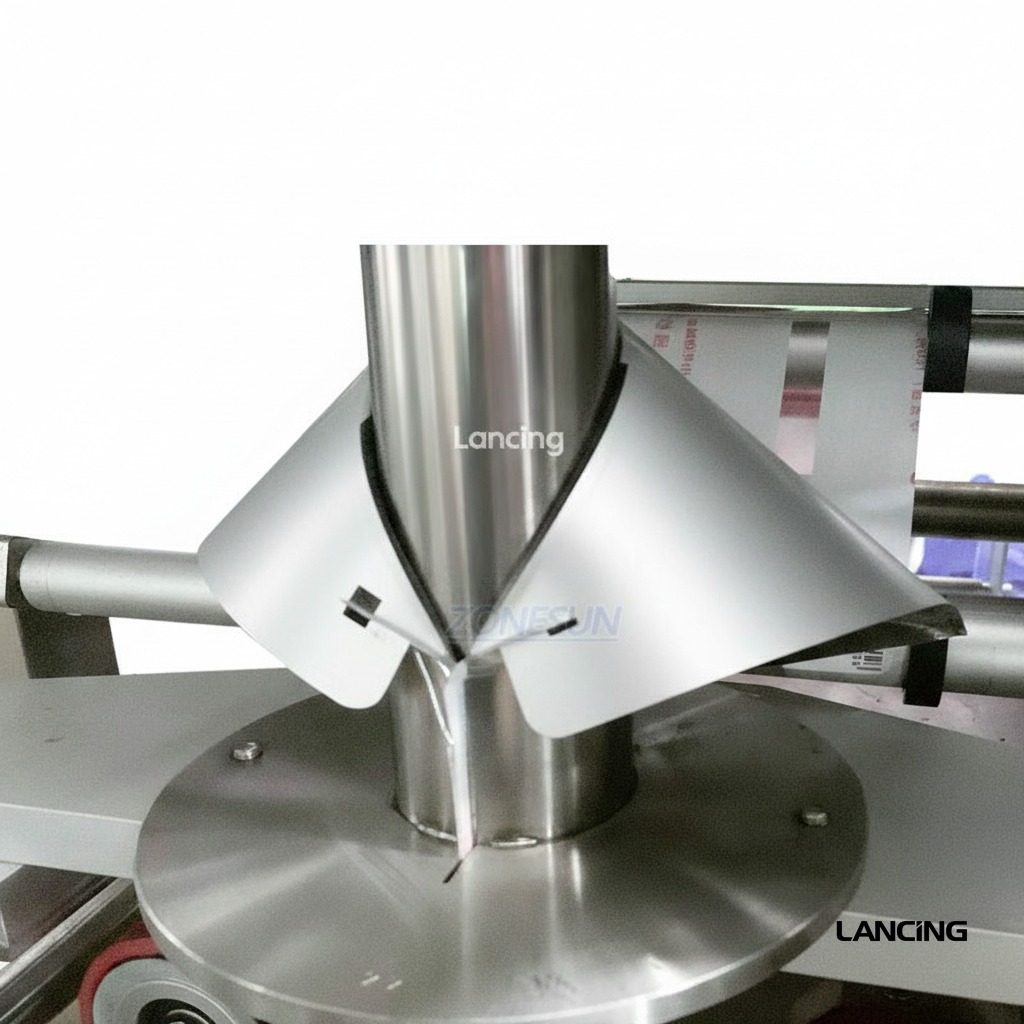
A VFFS route forms bags from roll film as part of the packing cycle. Provide reel and finished-bag details together, including material, print repeat and seal design. Compare film tracking, bag formation, dosing and sealing as one sequence. The required bag style and material behaviour may narrow the suitable machine arrangements.
A pouch-handling format does not determine whether auger, weighing, pump or another dosing route is appropriate. Trial powders with normal flow and dust, fragile pieces with realistic handling, and liquids with the intended temperature and nozzle cut-off. Keep the mouth and seal band clear under the same conditions.
Run the agreed format and material change, including replacement parts, settings and first accepted pouch. Count good filled and sealed packs after coding and inspection where included. Record replenishment and pauses as well as continuous running so quotations can be compared against the batch pattern the business actually needs.
A dependable pouch filling project starts with the product, the finished pack and the acceptance checks that will be used during trials. The machine name is only the starting point.
Provide the flat pouch width and height, usable opening, gusset dimensions, zipper or spout position, seal area, laminate structure and an actual pack sample where possible. For reel-fed VFFS work, include the film width, repeat length, registration mark and core details.
Product behaviour decides the dosing method. Flowability, bulk density, dust, particle size, viscosity, temperature, foaming, fibres and pieces can all change the filler, nozzle, hopper and product-feed arrangement.
Agree the target dose, permitted tolerance, saleable output, code position, seal appearance, leak-test method and changeover expectation before the machine is accepted. A representative product and production pouch are the best basis for a useful trial.
The figures below are published reference configurations. Actual output depends on product behaviour, dose, pouch or film, sealing dwell, coding, inspection and the wider line. Final values must be confirmed against the real application.
| Model | Reference route | Published fill or pack range | Published output | Useful format evidence |
|---|---|---|---|---|
| LU-FSK1000 | Granule weighing, bag filling and sealing | 50–1000 g, customisable | 5–15 bags/min | OPP, CPP, PE or PET film; reference roll width up to 420 mm and bag length up to 280 mm. |
| LU-FS02 | Back-seal granule VFFS | Approx. 20–1000 g, customisable | Approx. 20–30 bags/min, based on filling volume | OPP, CPP, PE or PET film; reference roll width up to 400 mm and bag length up to 280 mm. |
| LU-FS06 | Auger powder VFFS | 150–2000 ml | 5–80 bags/min | Reference bag size 60–250 mm wide by 80–350 mm long; maximum film width 520 mm. |
| LU-420GSY | Liquid and paste fill-and-seal | 100–1000 ml, customisable | Approx. 30–45 bags/min | Reference bag size 60–200 mm wide by 50–400 mm long; product and pump configuration must be checked. |
| LU-FSMP8 | Eight-lane liquid sachet VFFS | Reference sachet per lane: 15–26 mm wide by 34–150 mm long | Approx. 25–40 sachets/min per lane | Magnetic-pump dosing, back seal and a reference maximum film width of 500 mm. |
Use these values to frame an enquiry, not as a guaranteed production result. Lancing will confirm the relevant model, options and realistic rate after reviewing the product and pack.
A trial should prove more than whether product can pass through the filler. It should show that the complete cycle can produce repeatable, coded and sealed pouches that meet the agreed acceptance method.
Use normal production product, including the usual variation in temperature, bulk density, particles or viscosity. Send sufficient quantity for setup, parameter adjustment and a sustained sample run.
Supply printed or plain pouches and film with the intended laminate, zipper, spout, gusset and sealant layer. Small dimensional or material changes can affect opening, tracking and seal formation.
Review fill checks, seal appearance, code legibility, leakage method, reject conditions and changeover steps. Photographs or a short finished-pouch quality video are useful evidence when they are captured against an agreed test plan.
Lancing can use the real pack details to compare premade pouch, Doypack, VFFS, auger, weighing, pump and multi-lane routes without forcing the project into a generic machine category.
The fastest route to a useful proposal is to replace assumptions with a controlled pack brief, representative materials and an agreed way of judging the filled pouch.
For premade pouches, record the finished width, height, usable opening, gusset, zipper or spout location, seal area and laminate reference. For VFFS, identify the reel width, print repeat, registration mark, unwind direction, core and finished-bag dimensions. Normal manufacturing variation matters because the machine must handle a production batch, not one ideal sample.
Use the pouch material and laminate guide to prepare the packaging evidence.
Powder flow, granule fragility, liquid viscosity, temperature, foam and suspended particles influence the filler, feed system and nozzle or chute. The dosing method must remain stable through start-up, replenishment, pauses and restart, while keeping product away from the seal area.
Compare dosing-system selection factors before choosing the machine route.
Acceptance should cover dose, pouch dimensions, opening and gripping, seal appearance, code position, leak or integrity checks, reject handling and the output counted as good packs. A trial is more useful when the test method and pass criteria are agreed before materials arrive.
Plan seal and leak-test evidence for the finished pack.
Use the guides below to isolate pouch-handling, seal, coding, inspection and fault-finding requirements before they become late changes to the line.
These questions help separate the product, packaging and line decisions before a machine model is treated as the answer.
Fix the product and finished-pack requirements before fixing the model. The dosing principle, pouch-handling method and sealing process are selected from real product behaviour, pouch or film construction, target dose and the definition of a saleable pack. A model can then be shortlisted against those conditions rather than chosen from a headline description.
Start with representative product, a pouch or film drawing, production samples and the quality checks that will be used at trial. The pouch filling questions hub organises the next decisions.
Agree evidence for the product, pack, output and acceptance method. That normally means the product condition and dose range, pouch dimensions and construction, seal area, intended code, required good-pack output, utilities, line layout and the checks that decide whether a pouch is accepted or rejected.
This evidence prevents a technically possible fill from being mistaken for a complete production solution. Use the pouch filler specification checklist to record it consistently.
The pouch becomes the main automation risk when normal variation affects separation, opening, gripping or sealing. Zipper bulk, spout position, gusset folds, surface friction, stiffness, mouth width and supplier tolerances can all alter the handling window even when nominal width and height are unchanged.
A representative production batch should therefore be tested, not only one ideal sample. See what makes a pouch suitable for automatic filling.
The filler cannot deliver stable saleable output if product feed, coding, inspection, rejection or discharge cannot keep pace. A downstream blockage or missing ready signal can stop the pouch machine, while an unclear reject sequence can allow suspect packs to continue.
Review line states, accumulation and recovery before order so controls and mechanical interfaces are included in the scope. The line-controls guide explains the required decisions.
Send the application details, representative samples and required acceptance checks so Lancing can review the suitable pouch filling route.
A useful pouch filling shortlist needs three connected records: the empty pack and product input, the repeatable changeover method, and the evidence that will decide whether the installed line is accepted. Keeping those records together reduces assumptions between quotation, trial, build and handover.
Nominal pouch volume does not prove that the product will settle below the seal band. Record the intended dose, filled shape, foam or dust behaviour, zipper or spout position and the clean area needed for sealing.
Plan the pouch fill zone →List the change parts, recipe values, product-contact changes, film or pouch adjustments and first-off checks needed before the next format is released to production.
Build a changeover record →A factory test and site test should use the same agreed product, pack, good-pouch definition, fault challenges and evidence list, with site utilities and line interfaces added during SAT.
Define FAT and SAT evidence →These answers connect the finished pouch, the operating method and the acceptance evidence before a model is treated as the solution.
Fix the representative product condition, intended pouch or film, dose range, acceptable finished pouch and the checks that will be recorded. A demonstration can then test the real process rather than show only that the machine cycles. Include the normal product variation and a production batch of packaging where possible.
Headspace gives product time and room to settle while protecting the seal band from dust, liquid, foam or pieces. If the filled product reaches the jaw area, the line may need a slower dose, settling step, cleaning intervention or a different pouch geometry. The usable fill zone must therefore be trialled, not assumed from external dimensions.
Retain the approved product and pack references, setup values, fill results, seal checks, coding position, reject tests, changeover steps and accepted deviations. The evidence should remain traceable through machine build, factory acceptance and site acceptance so the agreed result does not change between stages.
Retest when a change can affect feeding, opening, filling, sealing, coding or the filled shape. That can include a new supplier, laminate, zipper, spout, print coating, pouch tolerance, dose, product condition or change part. The extent of the repeat test should match the process risk created by the change.
Include the product, packaging, intended fill zone, changeover matrix, output target and acceptance method so Lancing can review the complete route.
New pouch projects increasingly need a clear machine-layout choice, a controlled packaging-material transition and a documented cleaning boundary. These decisions should be tested against the real product, pouch and line rather than handled as catalogue assumptions.
Compare station sequence, footprint, dosing position, access and saleable-pack evidence before choosing the machine layout.
Compare premade pouch layouts →Separate recycling-design evidence from the handling and sealing tests needed to prove machinability.
Plan a material transition trial →Map product-contact parts, cross-contact risk, safe isolation, verification and first-off approval.
Define hygiene and cleaning →Lancing can review the material, machine layout, cleaning needs and evidence required for a useful trial and quotation.
A pouch-filling enquiry should start by stating whether the packaging format is already fixed. If printed premade pouches have been approved, supply the actual pack and its technical reference before comparing machinery. If the packaging is still being developed, ask the machinery and packaging suppliers to review the available routes together. This helps prevent a final artwork or pouch feature being approved before its handling and filling implications have been assessed.
Identify how the product enters the pack and how the pack will be closed. An open-top premade pouch, a spouted pouch and a bag formed from roll film should not be treated as the same purchasing task. Ask the proposal to show the supplied stages and the condition of the pack at each handover, including any opening, dosing, settling, sealing, capping or discharge operation.
Keep packaging samples traceable during the trial. Record the supplier reference, material version and relevant dimensions with the product and equipment setup. When the pack design changes, use that record to identify what needs review. A similar outward appearance is not sufficient evidence that the new pouch will behave the same way on the proposed equipment.
If the format is not already fixed, coordinate the packaging and machinery decisions. Obtain representative samples and confirm the proposed handling, filling and closing route before committing the production pack specification.